Because most of a job's time is spent waiting, usually at your bottleneck, here's how to use capacity planning to streamline your workflow without resorting to constant expediting.
Where does all your lead time actually go?
Most of it disappears into waiting, not working.
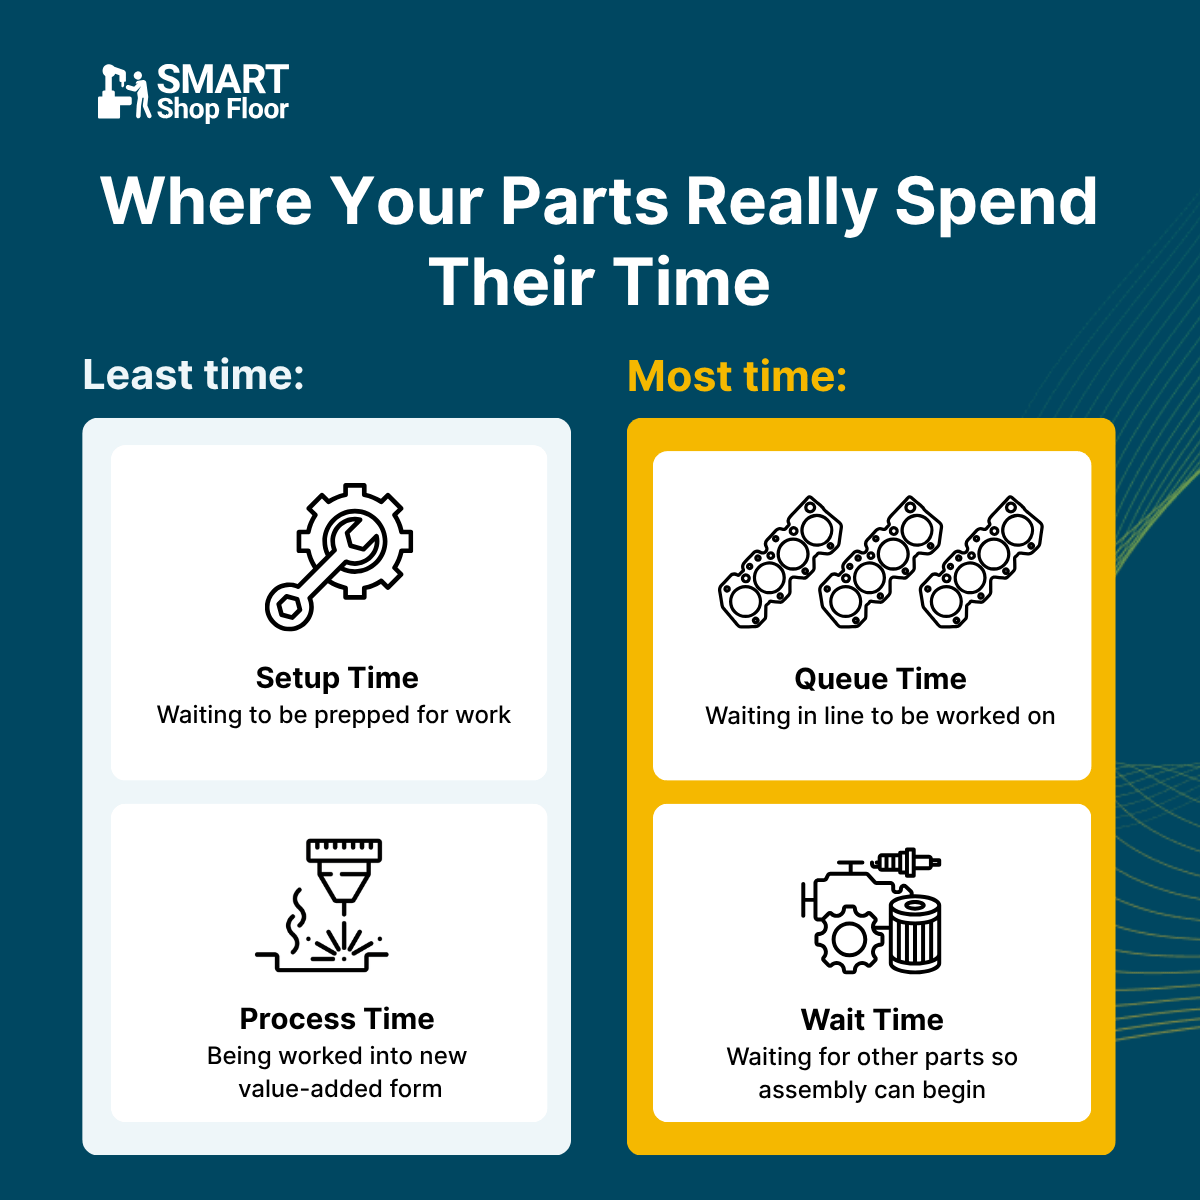
A job on your floor moves through four stages:
- Setup time: the time it waits for an operator to prep and begin work
- Processing time: the time actually spent turning it into a finished product
- Queue time: the time it waits in line because your people and machines are tied up with earlier work
- Wait time: the time it waits for other parts to catch up before assembly
Jobs spend most of their time sitting around waiting to be set up, worked on, assembled, or moved.
Processing, the actual work, is the smallest slice of the four. The old rule of thumb puts it at around 10% of total lead time.
The fix to shortening lead times and increasing throughput is eliminating wait time. To do this, you have two options:
- Carry less work-in-progress out on the floor
- Time the release of jobs so there's the narrowest possible window between start and due date
That's what automated scheduling does. It releases work exactly when it's needed, not so early it piles up at your bottleneck, not so late it blows the deadline. The result is smoother operations, shorter lead times and better on-time delivery rates.
Why is expediting rush jobs counterproductive, making lead times slower?
When lead times are running too long, or a rush order comes in, most shops expedite the job, jumping it to the front of the queue to skip the wait and get it out the door faster. Or they urge the team to work a bit faster that day. It works, for that one job.
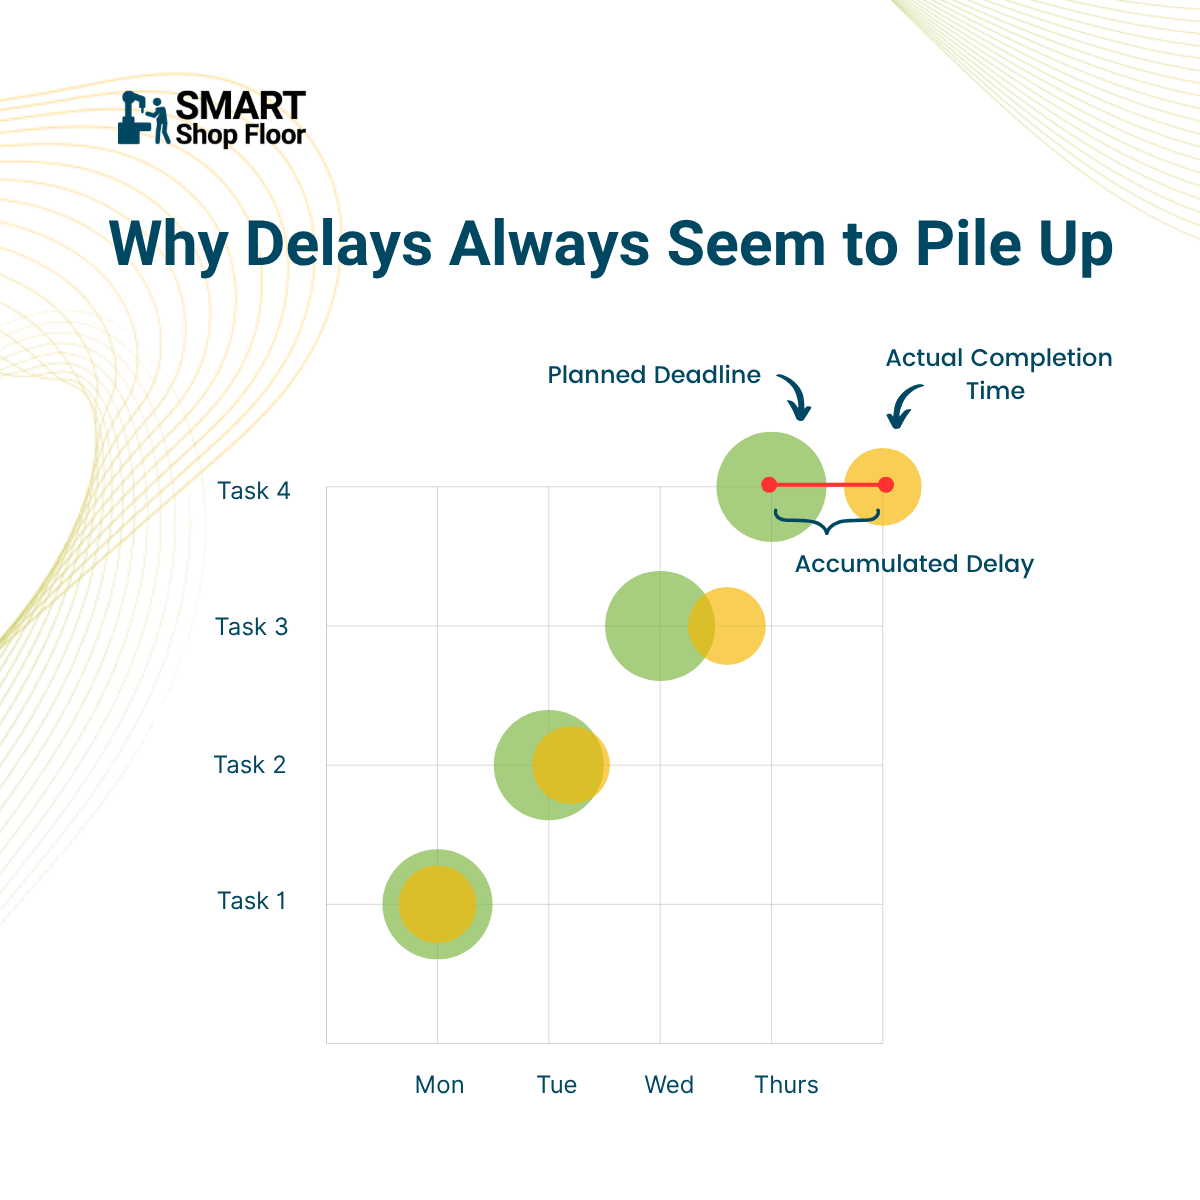
It's a misconception that when something runs slow, you can crank up the throttle elsewhere to make up lost time. Statistics show the opposite: jobs can only accumulate delays over time. Each process follows a set order, and you can't jumpstart work by skipping ahead. As delays build up and priorities get reshuffled, more of your time goes into sorting out problems instead of running the shop.
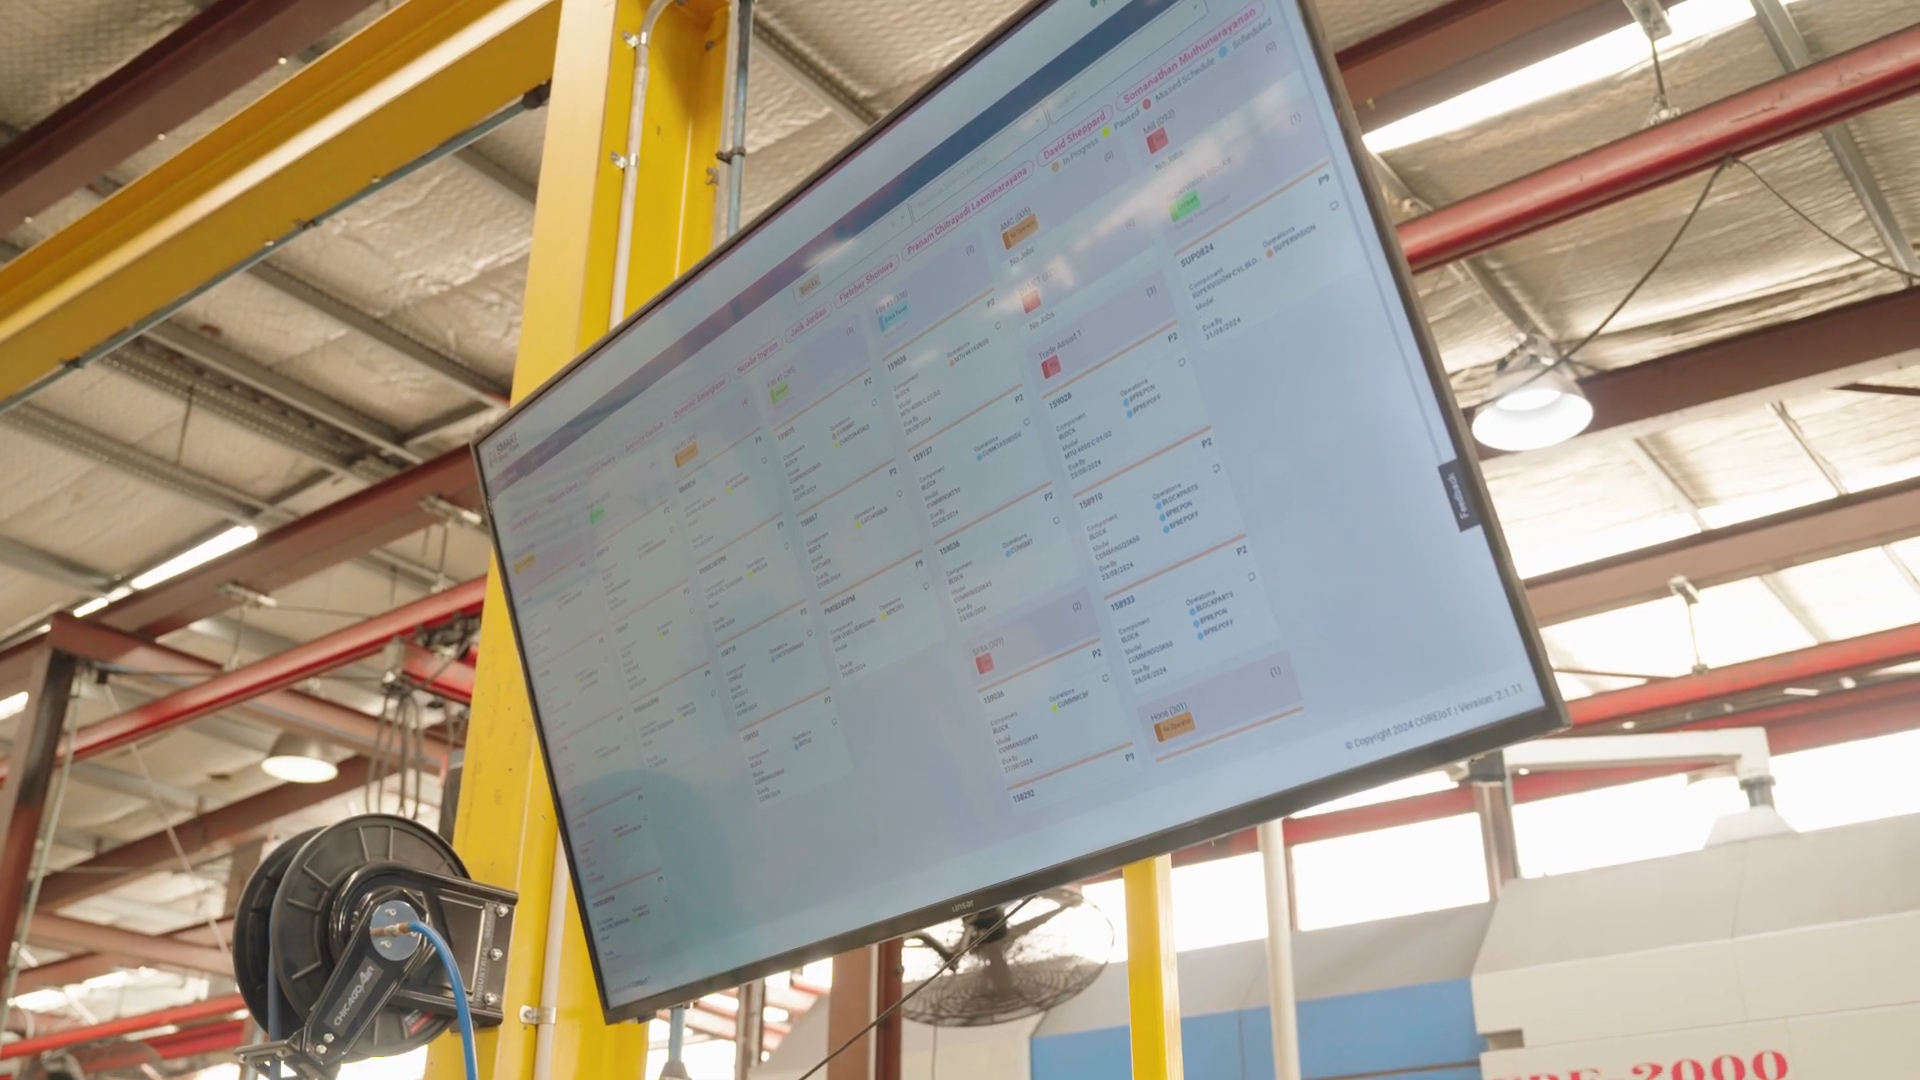
This is where the system needs to catch its own slippage, not your team. Smart Shop Floor identifies when delays mount and automatically reschedules work to recover. If a machine runs slower than expected, downstream schedules shift so another resource picks up the slack, and the rest of the plan holds.
Why does one bottleneck control your whole shop's output?
Because your bottleneck sets the pace for everything else.
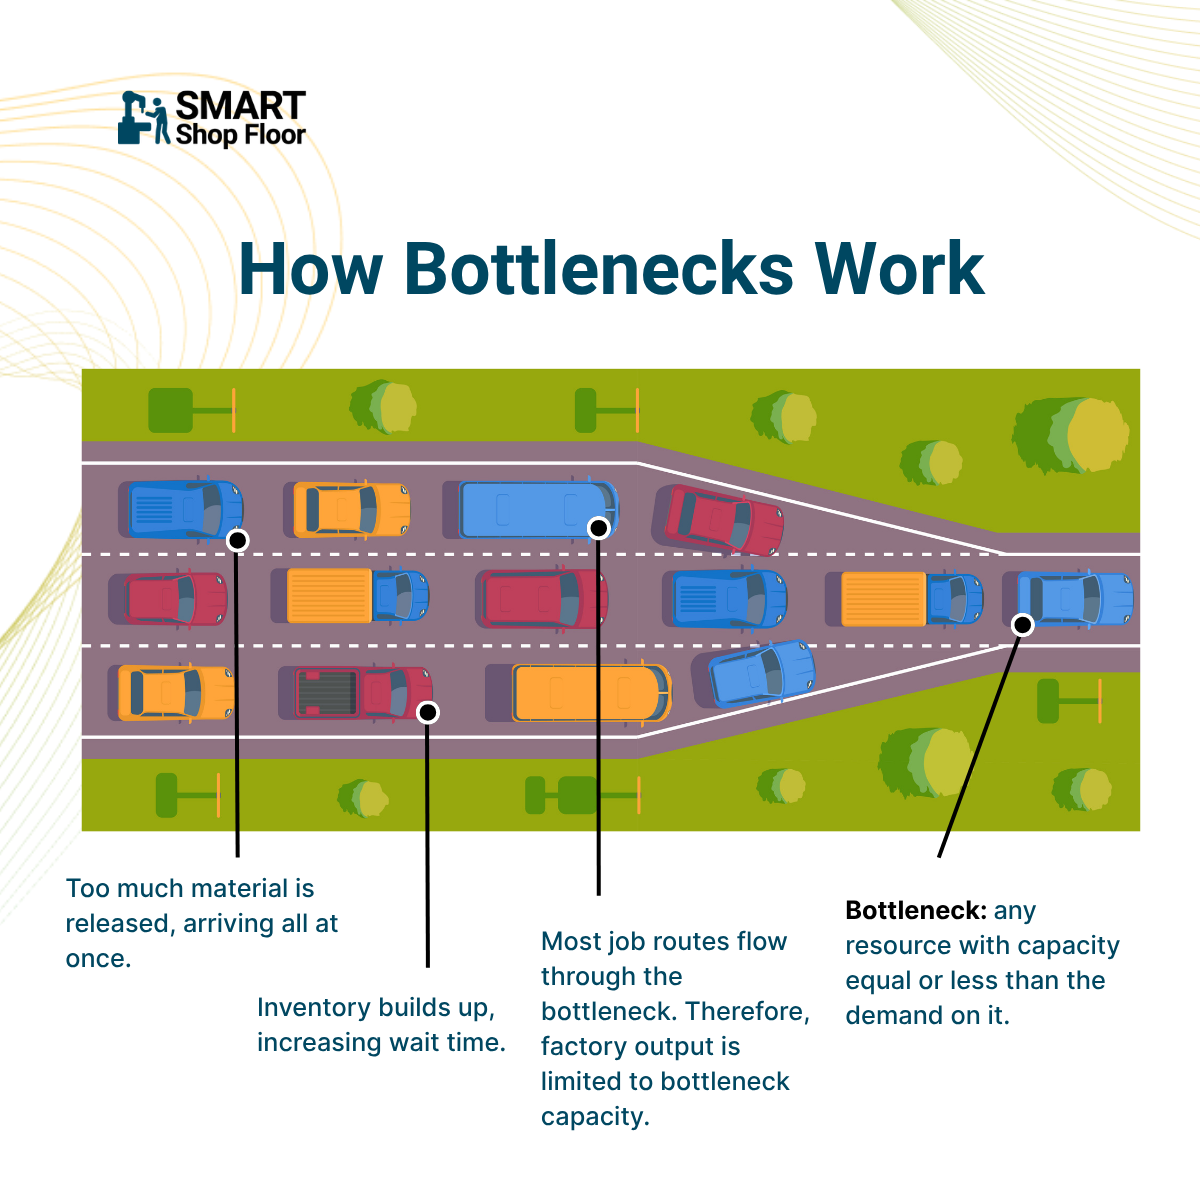
A bottleneck is any machine, station, or skilled operator where demand outstrips capacity. Most of your work has to pass through it, so your whole plant can only produce as fast as that one point allows.
Think of it like the merge on Highway 1 into Perth. Three lanes merging into one. Traffic backs up, engines idle, frustrated drivers lay on the horn. This single open lane limits everyone on the road.
With manual scheduling, too many new jobs get released and arrive at the bottleneck all at once. Work-in-progress piles up, wait times at the congested bottleneck grow, and downstream, machines and operators sit idle waiting for parts still stuck upstream.
Then the pile itself slows the bottleneck further, as operators waste time hunting for the next priority job and fighting for bench space.
Your bottleneck decides three things:
- How much your whole plant can produce
- When jobs should be released and how long lead times run
- How much inventory sits on your floor
Automated scheduling tackles the root problem by basing all decisions on your bottleneck's limits. It works backwards from that constraint. It releases only the inventory you actually need, times each job's arrival at the bottleneck, minimises the queue in front of it, and keeps it running at full capacity.
How do you use capacity planning to manage bottlenecks and grow your shop?
You stop trying to run every department at 100%, and focus everything on keeping your one constraint fed. The Theory of Constraints calls chasing full utilisation everywhere the "efficiency syndrome," and it costs you money. Departments that aren't your bottleneck can easily overproduce, and that extra work just sits as unfinished inventory, queuing behind the one resource that actually limits your output. Better to leave those departments some spare capacity, so they've got room to flex and support the constraint instead of grinding out WIP nobody can use yet.
Your bottleneck is the exception. Say cutting is your constraint. That machine and its operator need to be running flat out, constantly fed, never idle. If you see its capacity drop to 80 or 90%, that's not a minor dip, that's an urgent problem. The Theory of Constraints' golden rule is an hour lost at the bottleneck is an hour lost for the entire plant. A 10% efficiency drop there is a 10% hit to your total output.
Smart Shop Floor's Capacity Dashboard tracks capacity hours by machine or operator, so you can watch your bottleneck's day-to-day output and check how much of its future schedule is already booked out. When there's spare capacity sitting in the forward schedule, including at the bottleneck, that's your green light to chase more sales with confidence. When there isn't, taking on more work just means blown deadlines or overtime.
Understanding your true capacity, not just how busy everyone looks, is what makes growth sustainable rather than a gamble.