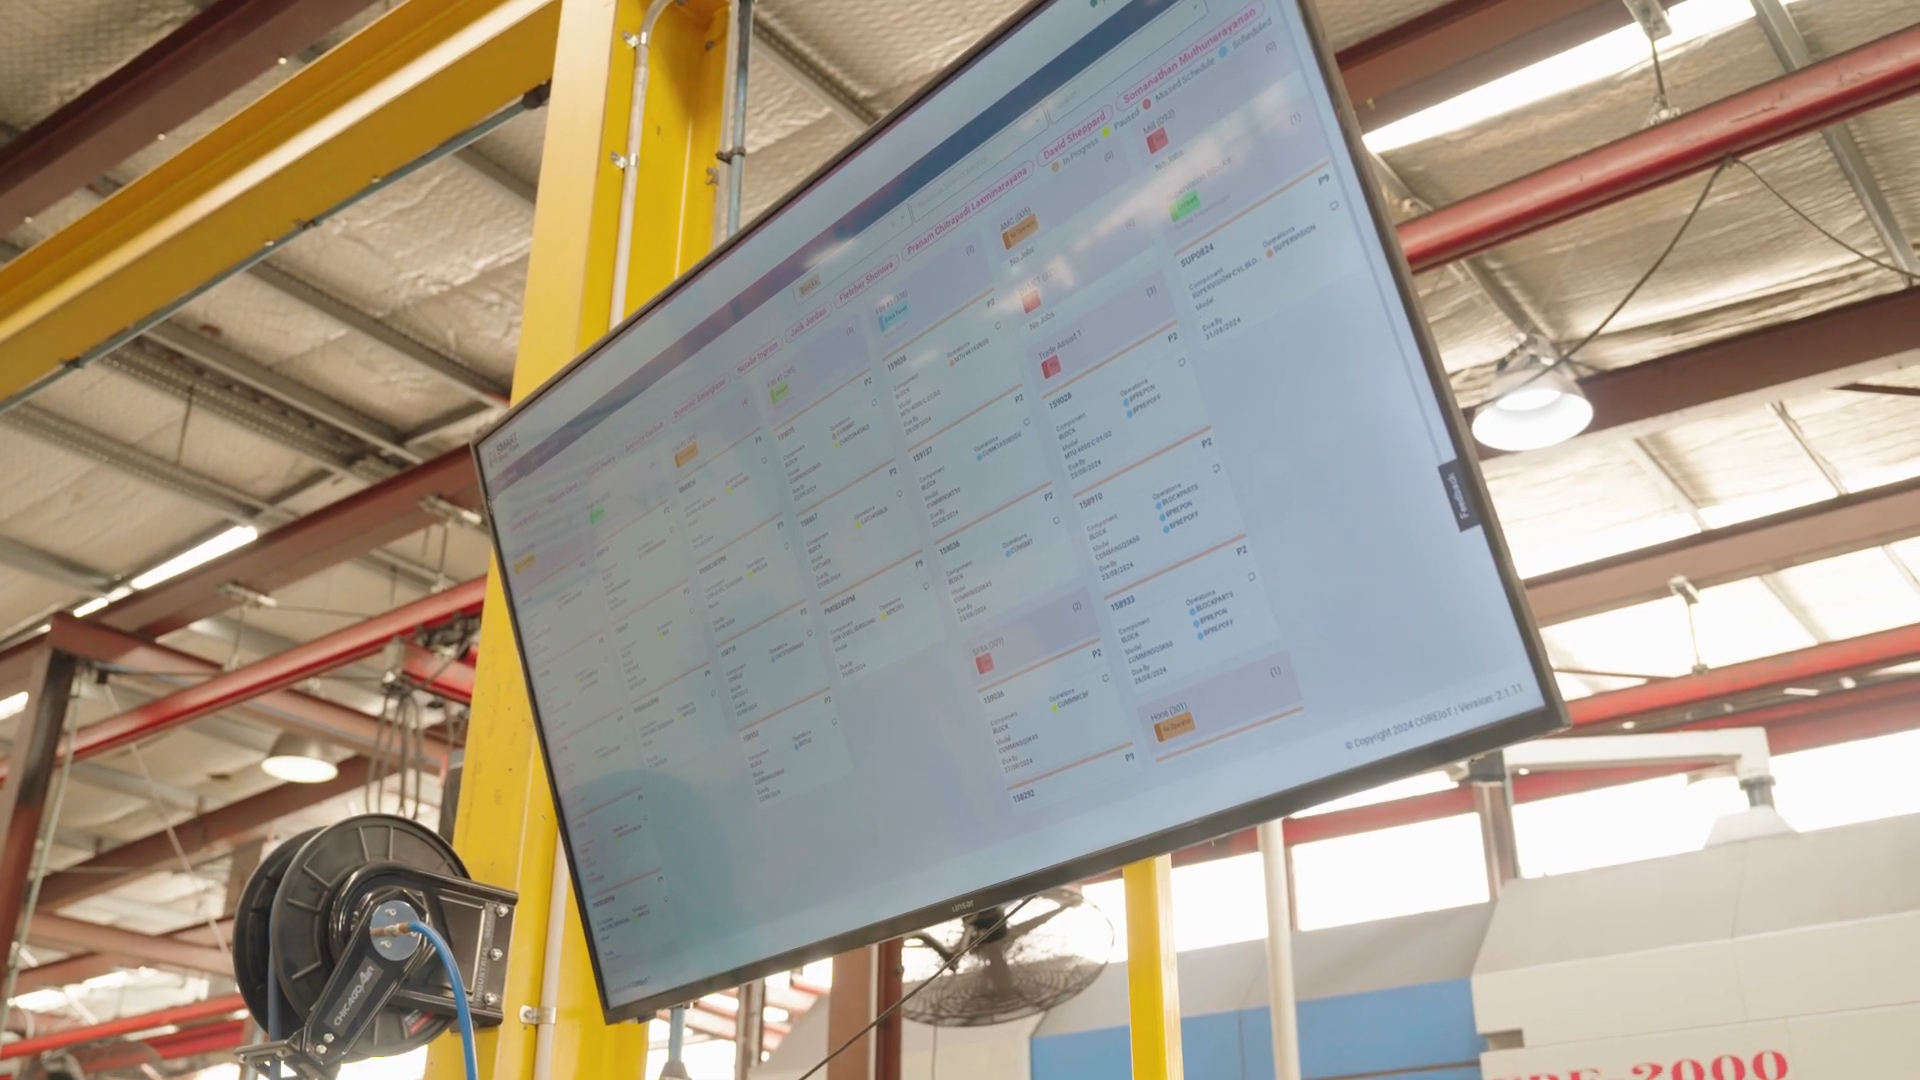
How an automated scheduling system decides what happens and when, the scheduling methods job shops actually use, and the business outcomes fabricators see once scheduling's automated.
Jump to:
Why production scheduling matters for job shops
What is automated production scheduling
The core components of an APS system
What Smart Shop Floor's schedule actually considers
Types of scheduling for job shops
What happens when a disruption hits
Why whiteboards, spreadsheets and ERPs fall short
Why mass-production scheduling doesn't work for job shops
The benefits of automated scheduling
Do you need an MES as well as a scheduler?
Real results from Australian fabricators
Why is production scheduling so important for job shops and fabricators?
In Theory of Constraints, the schedule is the pace-setter of a factory, called the drum: it sets the beat everything else in the shop has to move to. Get it wrong, and the plant either promises more than it can deliver, or crawls along with machines and people sitting idle waiting for work that never arrives on time.
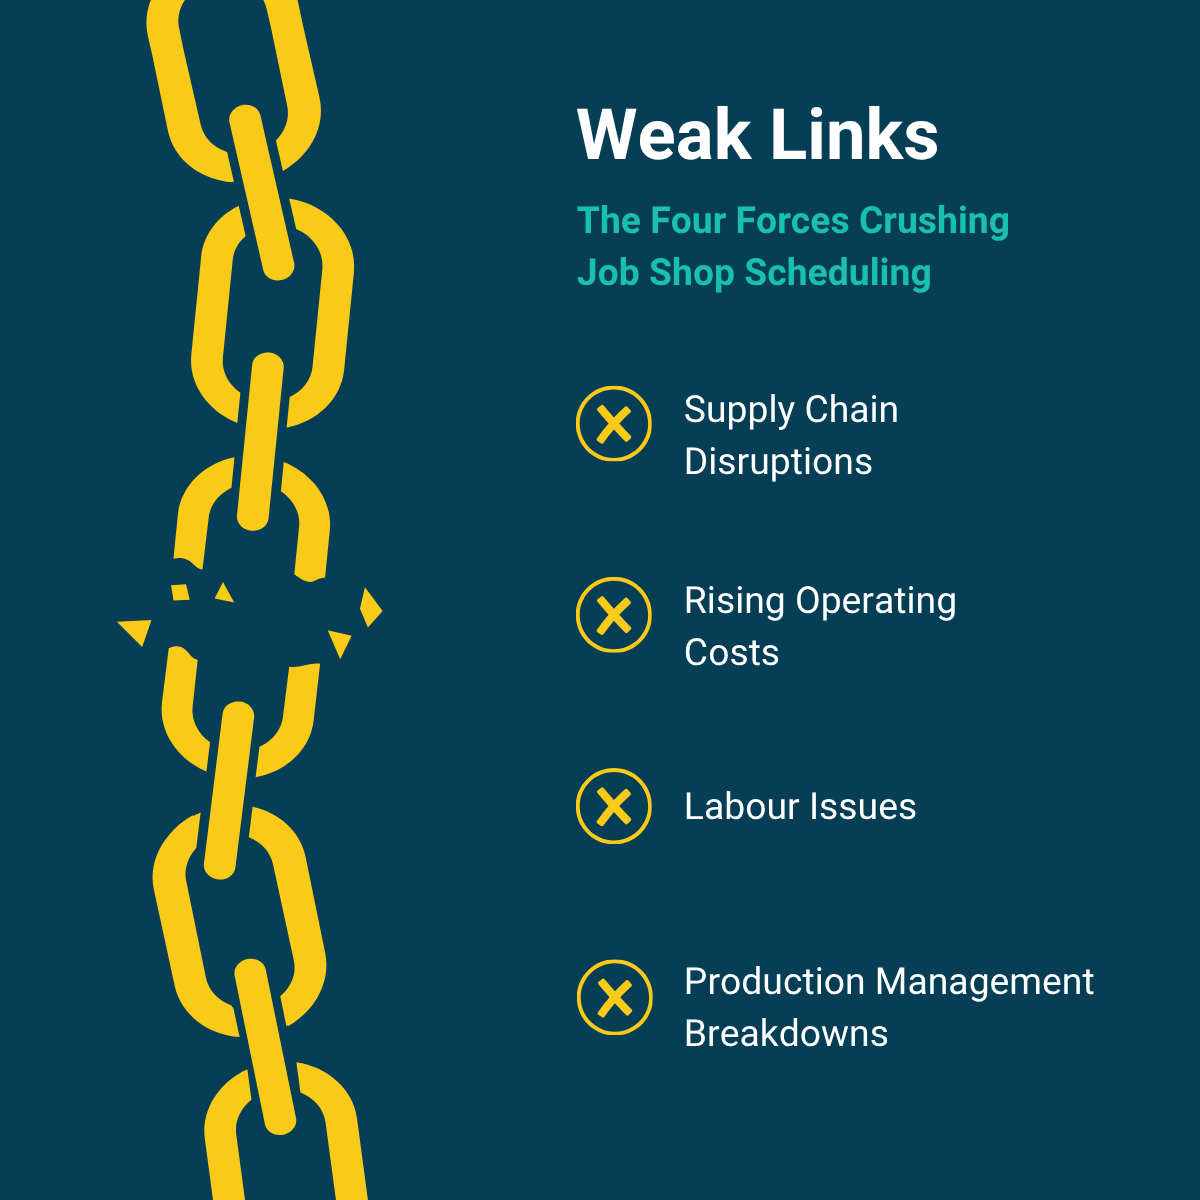
Three pressures are making that harder to get right across Australian manufacturing right now:
- Productivity keeps sliding. Manufacturing productivity has fallen 1% over the past decade. Manufacturing is sliding backwards while the country as a whole moves forward, with national productivity up 4.7% over the same period.
- Skilled workers are hard to find and hard to keep. Several factors are conglomerating to create this problem. Not enough new skilled workers are enrolling/graduating from training programs to keep up with demand, an aging workforce will see higher retirements in the coming years and skilled workers are being poached from manufacturing by higher paying industries.
- Input costs are climbing. Manufacturer input prices have risen 37.5% in five years, and 46% of manufacturing leaders now rank rising wage costs as their number one challenge for 2026.
Without a solid scheduling tool, job shops are struggling to:
- Use workers and other resources effectively, which means you're seeing overworked staff and underused machines
- Maintain accurate timelines, making it harder to meet deadlines
- Identify and resolve bottlenecks due to a lack of visibility throughout the factory floor
👉 READ NEXT: Australia's Manufacturing Productivity Crisis and the Technology Gap Behind It
What is automated production scheduling?
Automated production scheduling assigns specific people and machines to specific jobs over time. It considers due dates, processing sequences, and available resources to determine the optimal time for each operation.
At its core, scheduling is an optimisation puzzle: make the highest quality product in the shortest possible time, while working within real-world limitations.
A scheduling system is making several decisions at once:
- Releasing jobs for production
- Assigning resources (people, equipment, production lines) to tasks
- Reassigning resources from one task to another
- Prioritising tasks that need the same resources
What are the core components of an Automated Planning and Scheduling system for a metal shop?
An APS system runs on four parts, each working at a different timescale, from the whole year ahead down to today's shift.
Sales and operational planning (12–18 months)
This is the widest view: confirmed orders and quoted work sitting together on one calendar, showing exactly where capacity is open for new business and where the shop is already overextended. It turns quoting from a guess into a decision made against real remaining capacity, and gives enough runway to plan for people, machines or materials before a gap becomes urgent.
Master production scheduling (1–3 months)
This is the committed plan: a time-phased sequence of what gets built and in what order, checked against real capacity so it's achievable rather than a stack of due dates. Planned maintenance windows get reserved here too, treated the same as any other claim on capacity.
Material requirements planning
Running against that schedule, this works out what raw material and parts each job needs and when, so a shortage gets caught while there's still time to order rather than on the morning a job is due to start.
Work allocation (daily/shift)
At the sharp end, this decides who does the work: matching each task to a qualified, available operator, weighing the skills matrix and average completion time to choose the best fit for the job.
How they work together
Sales and operational planning sets the ceiling: how much new work the shop can actually take on. Master production scheduling sequences committed work inside that ceiling. Material requirements planning tests whether that sequence can run with available raw material, and flags any shortages so Purchasing can act before it delays a job. Work allocation puts people against the plan day by day, and if an operator's unavailable, that gets fed back up so the schedule adjusts before it costs a delivery date.
👉 READ NEXT: 4 Lessons from Automotive's Lean Supply Chain for Fabricators
What job shop inputs does Smart Shop Floor’s production schedule consider?
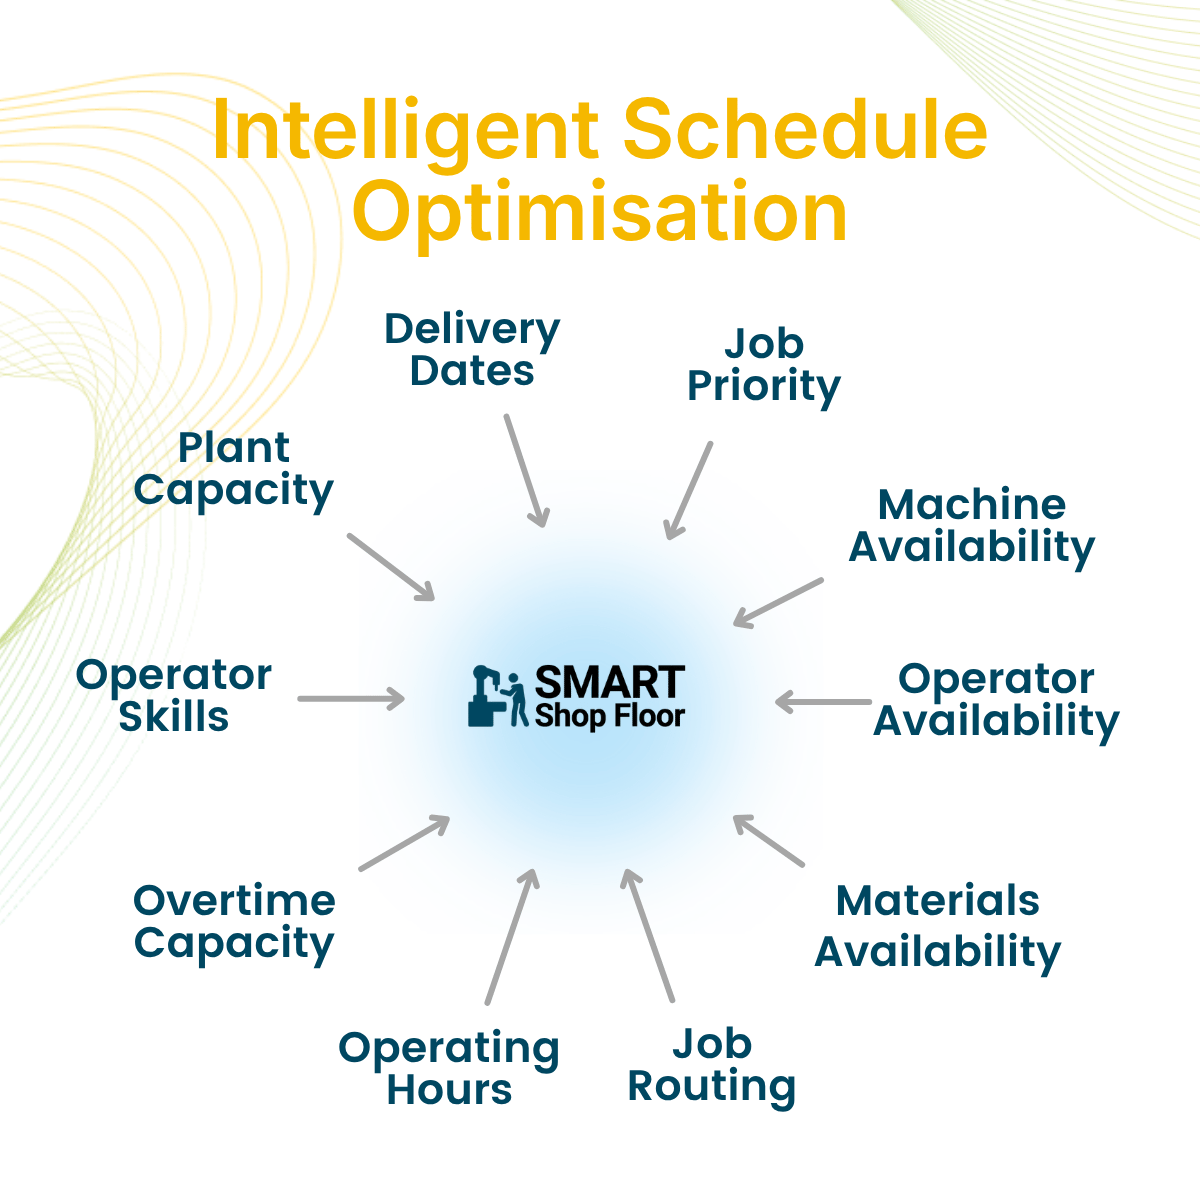
An automated production scheduling algorithm has to weigh a number of inputs in real time to decide what gets made, by whom, and when. These are the ten things Smart Shop Floor considers when building a schedule:
-
Delivery dates: customer required dates
-
Job priority: which orders take precedence
-
Operator availability: individual schedules, leave, sick days
-
Materials: raw material stock levels against Bill of Materials requirements
-
Machine availability: which machines are operational, scheduled maintenance, breakdowns
-
Operating hours: shift patterns, business hours, weekends
-
Overtime capacity: whether overtime is approved and available
-
Job routing: process sequence, operation times, setup times, dependencies between steps
-
Plant capacity: overall capacity and department-specific limitations
-
Operator skills: who's qualified to work on which tasks
That’s a lot of variables to consider. They have to be ranked in order to achieve the right outcomes: your best customers are taken care of, lead times are met, and labour is optimised to take advantage of available equipment and materials.
How Smart Shop Floor makes the call: step by step
- Due dates drive everything. It's the foundation, since every product's different and the customer's deadline is what matters most.
- When conflicts arise, priority levels decide what gets scheduled first. Assign priority to specific jobs or customers, and the most important work goes to the front of the queue.
- Two buffer types get built around that order, following the Theory of Constraints. Job-level buffers finish work hours or days ahead of the actual due date, so last-minute rushes don't happen. Operations buffers give operators a realistic cushion before each task starts, accounting for setup and moving between locations.
- Before anything locks in, someone gives the schedule a walkthrough. A drag-and-drop interface lets you tweak what the algorithm's proposed, and the system adapts everything else around the change.
- Jobs get assigned to specific operators, not just scheduled in the abstract, matched to the person best suited for the task.
- As jobs close out, that gets fed back in, updating the schedule and shaping what tomorrow looks like.
👉 READ NEXT: 5 Ways Automated Scheduling Fixes Manual Scheduling Challenges
👉 READ NEXT: How to Use Three Types of Time Buffers in Production Scheduling
What are the best types of scheduling for job shops?
Four scheduling methods come up most often in job shops: first-in first-out (FIFO), earliest due date (EDD), finite scheduling, and capability-based scheduling. Each solves a different part of the problem, and most shops end up combining more than one.
First-in, First-out (FIFO) scheduling
FIFO, first-in, first-out, also known as first-come-first-served, is one of the most basic scheduling rules. It's the same queuing rule used every day at retail and restaurants around the world: the first to arrive is first in line, and the first to get served.
In a FIFO job shop, orders are queued by date received and the job that arrived first is processed first (the exception, of course, is when sales makes a special request).
This can be paired with visual FIFO lanes, physical hold space reserved for work-in-progress that limits how many jobs can queue between processes. Think taped floor lines, markings on a roller conveyor, or designated shelf space. Once a lane is full, upstream work pauses to avoid overproduction. It only starts again once jobs advance and space opens up.
FIFO is the simplest scheduling rule to implement because it:
- Reduces priority conflicts by avoiding jumping quick or "important" jobs to the front
- Simplifies task management since operators always know which job is next
- Prevents work-in-progress backlogs and bottlenecks
But it has limitations. In a high-mix environment with lots of customisation, it doesn't optimise for due dates or setup times. A job with a fast turnaround gets stuck waiting its turn and could miss its due date through no fault of the shop, it's just the rules of the game. And similar jobs aren't grouped together, meaning you're switching back and forth between setups.
Earliest Due Date (EDD) scheduling
Earliest Due Date, also called Earliest Deadline First, uses one piece of information: the job's final due date. You schedule the job with the earliest due date for production first, so it's ready to go.
Unlike first-in first-out scheduling, EDD is dynamic. The production queue changes as new orders come in to accommodate jobs with the closest deadlines. This method can be done using a spreadsheet and some basic filtering criteria, making it a popular choice for SME job shops and fabricators.
The real benefit is that it improves on-time performance and reduces maximum lateness. In plain English, your late jobs will be less late. Instead of a job being 10 days overdue, it might only be 2 days behind.
Smart Shop Floor uses a more advanced variant of this rule, called Earliest Operation Due Date (EODD). This version breaks jobs down into individual operations and calculates a separate due date for each step. This way, the scheduling software can:
- Spot delays early, showing the expected completion time so you can add overtime or an extra shift before missing the due date
- Account for travel and prep time between operations
- Handle complex interdependencies, analysing your workflow to manage jobs with shared resources and varying task lengths
It's the difference between only knowing an order ships Friday, and understanding the full workflow with cutting starting Tuesday morning, welding beginning Wednesday afternoon, and powder coating happening Thursday, so each department has what it needs when it needs it.
Finite scheduling
Finite scheduling only plans work your shop can actually complete with the machines, time, people and materials you have available. It's the opposite of infinite scheduling, a common flaw in many production systems that assumes unlimited resources, which is why a carefully planned schedule can fall apart by lunchtime.
Infinite scheduling is more commonly used by ERPs and generic scheduling tools because it's simpler to calculate and doesn't require on-floor touchpoints to capture real-time data. This can be sufficient for high-volume manufacturers with stable demand and repetitive production, but for a fabricator handling unique customer orders, infinite schedulers load work based generally on due dates and materials, which can create impossible workloads and unrealistic delivery promises.
It's like planning a road trip based on how much fuel is actually in the tank, rather than assuming an unlimited supply.
This type of scheduling is purpose-built for job shops and custom manufacturers and can handle:
- Varying order quantities
- Differing lead times
- Diverse product routings
- Customized bill of materials
- Shifting due dates
Capability-based scheduling
Capability-based scheduling assigns tasks to operators based on their skills and proficiencies.
Say you've got a priority order for some custom sleeves, and two operators qualified to do it:
-
Frank - proficient welder, ranked 4/5 stars
-
Hassam - your senior welder, ranked 5/5 stars
Unless you're standing on the floor with a stopwatch and a clipboard, you have no real way of knowing who's actually fastest, who's improved, or who's dragging their feet.
Smart Shop Floor quietly calculates variance analysis, so the system knows Frank averages 32 minutes to complete his jobs, while Hassam does it in under 25. Combine proficiency with speed and Hassam automatically gets assigned the upcoming job, ensuring everything is finished in the time available.
What happens when an unforeseen problem delays the production schedule?
Rescheduling is the process of updating an existing production schedule in response to a disruption, while still working to hit deadlines. Plenty can trigger it: machine failures, processing delays, rush orders, quality problems, or unavailable material.
With a manual schedule, every one of those turns into firefighting. Every operator has to be updated, with work stopping and being shuffled around. There's also a big difference between an optimal schedule that gets the most done and a workable one that just barely keeps things on track.
What sets automated scheduling apart today is its ability to reschedule in real time, captured through sensors and operators logging activity on tablets, rather than waiting for someone to notice and manually redraw the plan. It finds the optimal schedule in a fraction of the time and pushes out the updated work assignments to operators without requiring an all-hands meeting.
👉 READ NEXT: Why Your Bottleneck Runs Your Capacity (And How to Reverse It)
Why do whiteboards, spreadsheets and ERPs fall short as scheduling solutions for metal fabricators?
Whiteboards, spreadsheets and ERPs all break down the same way: none of them adapt automatically once something changes on the floor, so a person has to notice the problem and manually rebuild the plan every time. Job shops have been scheduling the same way for decades regardless: assembling a list of hot jobs and working top to bottom. Henry Gantt invented his still-popular production control chart back in the 1920s, and a century later, enterprise ERPs that rolled out in the 1990s still only offer incomplete scheduling capabilities.
Whiteboards
Whiteboards are popular for good reason: they're visual, cheap, and easy to update on the fly. The problem isn't the concept, it's what happens after the update. Information goes out of date the moment something changes elsewhere in the shop. Handwriting gets wiped by accident, taking the only record of a job's status with it. And there's no way to see who made a change, or when, so there’s no work history available.
Spreadsheets
A spreadsheet can sort jobs by due date well enough. What it can't do is adapt automatically: when a job runs late or a machine goes down, nothing recalculates on its own, the scheduler needs to update every downstream job by hand. And it can't calculate a realistic completion time once delays are added into the mix, only ever the number entered when the sheet was first built.
ERPs
Most ERP scheduling modules run on rough-cut capacity planning: it spreads work across the month without checking whether you've actually got the machines, people or time to do it. That works for high-volume, repetitive production. It doesn't work for a job shop juggling different routings, setup times and skills on every job. ERPs were built to run the money side of the business, not the floor, so scheduling gets added on afterwards. When a machine breaks down or material doesn't arrive, there's no feedback loop telling the system what's actually happening, so someone has to rebuild the plan by hand. And that's before the cost and months of implementation it takes just to get an ERP scheduling module running in the first place.
Why doesn't mass-production scheduling work for job shops and fabricators?
Most scheduling software, including the free or budget options, is built for repeatable manufacturing: the same product, run after run, on a predictable line. That's a fundamentally different problem to a job shop or metal fabricator running a different job, with a different routing, for a different customer, every single day.
| Mass / repeatable production | Low volume, high mix / non-repeatable | |
| Product mix | Same product, run after run | Different job, different spec, every time |
| Scheduling logic | Infinite capacity: assumes resources are always available | Finite capacity: only plans what machines, people and materials can actually deliver |
| What drives the plan | Volume and throughput targets | Due dates and job priority |
| Routing | Fixed, predictable sequence | Changes job to job |
| Setup and changeover | Minimal, same setup repeated | Frequent, different setup per job |
| Demand pattern | Stable, forecastable | Unpredictable, customer-driven |
Job shops need scheduling that handles varying order quantities, differing lead times, diverse product routings, customised bills of materials and shifting due dates, none of which a system built for repeatable production was ever designed to do.
What are the benefits of automated production scheduling for job shops?
On the floor:
- Clear daily priorities on a tablet, no chasing down a supervisor for the next job
- All the information operators need in one place, with quick digital paperwork instead of hunting for the right form
Across the shop:
- The schedule adjusts itself when a machine goes down or a job runs long, instead of someone reworking it by hand
- Skilled operators and machines stay in use, not idle waiting on the next job
- Overtime gets minimised, saving on costs
- Inventory accuracy: shortages get caught while there's still time to order, and cash doesn't sit locked in excess stock you didn't need
- Work-in-progress moves through the shop faster, cutting production time instead of piling up at the bottleneck
For the business:
- Real-time job costing replaces guesswork on what a job actually cost to run
- Due dates you quote are due dates you actually hit, a genuine edge when quoting new work
- Fewer phone calls chasing job status, customers get their own live view instead
- Scheduling scales with the business, instead of becoming the ceiling on it
- Less pressure on the people running the floor day to day
👉 READ NEXT: How Fabricators Can Win the Fight for Skilled Workers
Do fabricators need a manufacturing execution system as well as a production scheduling tool?
It depends on how much control and visibility the business wants over what's actually happening on the floor. MES isn't a new system to learn, it's the same platform going a layer deeper. Scheduling organises the plan; MES manages how that plan actually gets executed on the floor.
- Manages, monitors and synchronises work execution from raw material to finished product
- Tracks work-in-progress, machine performance and labour in real time to keep the plan on track
- Connects your ERP with what's happening on the floor for complete visibility
- Surfaces bottlenecks and inefficiencies a spreadsheet won't show you, growing capacity and shrinking lead times
How it works in practice:
Operator interface
A dedicated app puts work instructions, drawings, quality checks and messaging in operators' hands, so questions get answered without a walk across the floor.
Job status logging
Operators log work progress with a single tap, tracking work time, downtime reasons and job status as it happens, not reconstructed at the end of the day.
Uptime monitoring
Tracks machine uptime and operator productivity in real time, showing exactly where time's being lost before it eats into a delivery date.
Digital forms
Quality checks, maintenance logs and safety records get filled in on a tablet and timestamped automatically, replacing paperwork that gets lost or filled in from memory at the end of a shift.
👉 READ NEXT: Shop Floor Control: Know Where Every Job Is Without Walking the Floor
Does automated scheduling actually work for Australian fabricators?
R. Moore and Sons found manual scheduling wasn't cutting it. With 70 staff running over 150 machines and 500 components, they were managing more than 8,000 possible combinations in their daily workflow. As orders grew, manual scheduling created confusion, fast.
Smart Shop Floor integrates with their ERP and keeps a running tally on machine availability and staffing. Pulling released jobs from a single source of truth, the algorithm slots work according to priority, labour availability and ready materials, then assigns jobs to the fastest and most skilled operators.
"It tells us what parts we need, when the ETA due date is, and schedules it all for us without us having to work that out manually with a team leader," said Chad Geary, Service Manager. Managing Director Stuart Davis said being able to concentrate on the work itself, not the scheduling, has helped move the business forward: it "has really lowered the stress level".
Watch R. Moore & Sons' story →
A.D. Coote & Co, an Australian sheet metal manufacturer with more than 55 years in business, saw a similar shift. After a year running Oracle NetSuite alone, the shop floor was still dragging: inherited manual processes had staff duplicating, sometimes triplicating, work.
Since adding Smart Shop Floor alongside NetSuite, they've reported:
- Scheduling flexibility. The team can adapt in real time to shop floor conditions and see the production impact of a maintenance or staffing change before deciding how to handle it.
- Hours saved daily. Their production manager saves hours every day with no more manual schedule revisions and instant answers ready for customer enquiries. Operators save hours too, avoiding formerly typical production delays.